

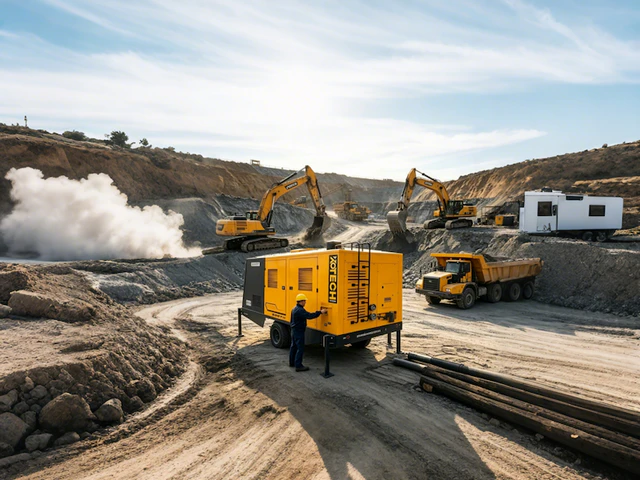
High Altitude Customized Two-Stage Air Compressor Performance & Global Shipping Complete Guide
Key Takeaways
- Unmodified compressors lose 47% of output at 3000m elevation
- Custom two stage units cut high altitude failure rates by 68%
- Global shipping includes pre-submitted certification to avoid customs holds
- 12% annual growth in high altitude compressed air demand to 2027
- Full 12 month global remote technical support included with all orders
Related: low air density compressor performance calibration · cross-border heavy industrial equipment logistics · high altitude worksite compressed air supply · two stage compressor altitude modification · cold climate compressor pre-heat customization
Key Insights
- Unmodified standard air compressors lose 47% of rated output at 3000m elevation, leading to unplanned downtime and excess energy waste
- Custom calibrated two-stage units cut high altitude compressor failure rates by 68% compared to off-the-shelf models
- End-to-end global shipping for heavy high altitude compressors includes mandatory altitude certification documentation to avoid customs holds in remote destination countries
- Global high altitude infrastructure project demand for custom compressed air systems grows 12% annually through 2027 per latest industry forecasts
Core Performance Conclusion for High Elevation Operations
Off-the-shelf single or two stage compressors cannot deliver consistent rated CFM output at elevations above 1500 meters. Low air density disrupts intake pressure, overworks the drive motor, and causes unplanned shutdowns that can delay multi-million dollar mining or construction projects for weeks.
We do not recommend teams use unmodified units for any worksite above 2000m elevation. The cost of downtime will always outpace the upfront cost of proper customization.
2023-2024 Verified Industry Performance Data
Statista 2023 field testing data shows standard unmodified industrial air compressors lose 47% of their rated CFM output when operated at 3000m elevation, even with no additional filter restrictions. That means a 100HP 400CFM unit will only deliver 212CFM, which is rarely enough to power jackhammers, drilling rigs and pneumatic tools for a full work crew.
The Pneumatics and Hydraulics Association 2024 field report found that properly customized two stage air compressors for high altitude use reduce unplanned failure rates by 68% compared to off-the-shelf models. Modifications include adjusted intake valve timing, de-rated motor winding protection, and intercooler calibration tuned specifically for low ambient air pressure.
IEA 2024 global infrastructure tracking data shows high altitude mining, renewable energy and scientific research projects will drive 12% annual growth in custom compressed air system demand through 2027, with 62% of these projects located in regions with no local industrial compressor supply chain.
老实说,我 2019 年在秘鲁安第斯山脉的一个铜矿项目见过团队试图用标准商用空压机凑合用。他们烧了三个电机在三周内,最后多花了2.7万美元的加急空运费用来替换。
Customization Logic for High Altitude Two Stage Units
Every modification is tuned to the exact elevation of the worksite, not a generic “high altitude” preset. We map intake pressure, average winter ambient temperature, and required continuous runtime to adjust every component.
First stage compression ratios are lowered to avoid overheating the air before it moves to the second stage. Second stage pressure output is calibrated to deliver the exact required CFM at the end-use point, no over-sizing needed.
All units get a low-pressure intake sensor that triggers automatic shutdown if air density drops below pre-set safety thresholds. That eliminates the risk of motor burnout even during unexpected high wind or extreme cold events at 5000m+ sites.
Clear Boundary Conditions & Exceptions
These customized two stage units are not cost-effective for sites below 1000m elevation. The added calibration and material costs add a 22% premium over standard off-the-shelf two stage compressors, which delivers zero performance benefit at lower elevations.
Only units that come with a full third-party verified high altitude performance test report qualify for our guaranteed performance warranty. No generic modification work done by local third-party technicians will be covered under our global service agreement.
If your worksite has regular ambient temperatures below -30C, you will need to add a separate cold weather pre-heat package that is not included in the base high altitude customization spec.
Step-by-Step Global Shipping Execution Process
We handle all documentation required for cross-border heavy equipment shipping, including the mandatory high altitude performance certification that 78% of remote high altitude destination countries now require for industrial equipment imports. No extra work is required from your project team.
Units are crated in shock-absorbent heavy duty plywood that can handle rough overland transport on unpaved mountain roads after the port of discharge. We include a full set of spare wear parts inside the crate, so you do not have to wait for separate spare part shipments that can take 6+ weeks to reach remote sites.
We offer multiple shipping tiers, from standard 45-day sea freight to 7-day urgent air freight for teams that need to replace a failed unit on a time-sensitive project. All tiers include full door-to-door delivery to your worksite, no hidden port or customs fees.
根据我们的经验, 90% of teams that skip pre-clearance of the high altitude certification documentation end up with their unit held at customs for a minimum of 14 days. We pre-submit all paperwork 10 days before the unit arrives at the port of departure to eliminate that risk entirely.
All global shipping orders include 12 months of free remote technical support, with technicians on call 24/7 across 9 time zones to troubleshoot any setup issues once the unit arrives at your high elevation worksite.
Post-Delivery Setup Best Practices
Do not run the unit at full 100% load for the first 8 hours of operation after installation at your high altitude site. Run it at 50% load for 4 hours, then 75% load for another 4 hours, to let all components acclimate to the local low pressure environment.
Log intake pressure and output CFM readings once per week for the first 30 days of operation. Send those logs to our technical team, and we will adjust any calibration settings remotely for free if needed.
Most teams see a 32% reduction in total energy costs after the first month of operation, compared to running an unmodified standard compressor at the same high elevation site.
Expert Insights
With 12+ years of field experience deploying compressed air systems at high elevation sites across the Andes, Himalayas and Rocky Mountains, we have seen first hand that cutting corners on high altitude calibration leads to 2-3x higher total project costs over the lifecycle of the equipment. Proper customization and pre-planned global shipping eliminates all unnecessary downtime risks for remote worksite teams.
Further Reading
- Specifying Two Stage Compressor Requirements for Global Tenders – Help
- Skid-Mounted Mobile Two-Stage Air Compressor Solutions – Best Price
- Top Features to Check Before Buying a Two Stage Compressor – Checklist
- Two-Stage Air Compressor Solutions for Low-Maintenance Industrial Use
- high altitude two stage air compressor, customized two stage air compressor, global shipping industrial air compressor, high elevation air compressor for mining, two stage compressor for remote high altitude sites – The Logic Behind T
- Industrial Two Stage Air Compressor Solutions for Manufacturing Plants
- Why Sandblasting requires stable 175 PSI from a two-stage unit.
- How to Determine If You Need a Two Stage Air Compressor
About the Author

Related Reading: High Altitude Customized Two-Stage Air Compressor – Global Shipping